Machine Vision Camera in Melbourne
Join industrial buyers comparing supplier quotes and buying with confidence. Free, quick and easy.


How IndustrySearch works
Tell us what you need
Answer a few quick questions about the equipment you're looking for.
Get personalised quotes
Receive tailored quotes from relevant Australian suppliers.
Compare and choose
Compare quotes, ask questions and choose the best option for you.
 Save time
 Compare quotes
 Buy with confidence
Save time, compare quotes & buy with confidence
Machine Vision Camera Suppliers in Melbourne
Diverseco is an Machine Vision Camera supplier to Melbourne
Originally evolving from the industrial weighing sector, Diverseco has built on its capabilities to become one of Australasia’s leading measurement and automation solutions providers to organisations in a broad range of industries. Diverseco’s primary objective is to deliver its customers superior value by combining an intimate understanding of their needs with our problem-solving ...Customers: Toll Logistics, Remondis, Cleanaway, Tox Free, GWF, Nestle, Boeing, Toyota Motor Company
Micromax is an Machine Vision Camera supplier to All
Micromax Pty Ltd is a long-established Australian technology supplier with over 65 years of continuous operation, specialising in embedded computing, ruggedised systems, medical computing, industrial communications, power solutions, and custom engineering services. The company services critical industries including healthcare, defence, mining, utilities, telecommunications, ...Customers: Woolworths, Optus, Vodafone, SMEC Australia, Saab Australia, Design to Production

Portable Analytical Solutions Pty Ltd is an Machine Vision Camera supplier to All
Established in 2009, Portable Analytical Solutions delivers comprehensive knowledge and support across an extensive range of instruments and applications. Working with XRF, NIR, LIBS, Hyperspectral and FTIR technologies, and with experience in the development of analytical solutions, PAS has an intimate knowledge of the specific product to suit what you need to do. We get ...
Teledyne FLIR is an Machine Vision Camera supplier to Melbourne
Teledyne FLIR designs, develops, manufactures, markets, and distributes technologies that enhance perception and awareness. We bring innovative sensing solutions into daily life through our thermal imaging, visible-light imaging, video analytics, measurement and diagnostic, and advanced threat detection systems. Teledyne FLIR offers a diversified portfolio that serves a number ...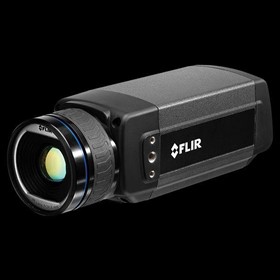
Vision Systems Engineering is an Machine Vision Camera supplier to Melbourne
Vision Systems Engineering (Aust) provides practical solutions for automatic product inspection, measurement, sorting and machine vision requirements. We offer no-obligation feasibility trials, showing images of your product being inspected with measurements and statistics to support the findings. We integrate computer controlled complex vision systems as well as smart cameras ...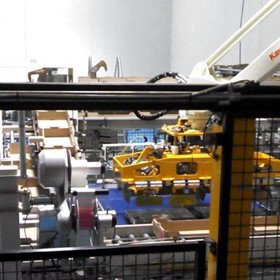
SciTech Pty Ltd is an Machine Vision Camera supplier to Melbourne
Scitech Pty Ltd is a leading supplier and systems integrator of specialised instrumentation, software and peripherals for the research, biomedical, life science, physical science, pathology, manufacturing, defence, government organisations and industrial communities. Scitech's attention to detail provides professional satisfaction and underpins our commitment to delivering ...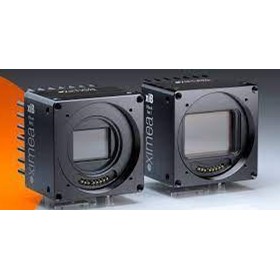
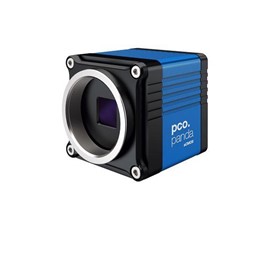
Datalogic Australia is an Machine Vision Camera supplier to Melbourne
Datalogic is a global technology leader in the automatic data capture and factory automation markets, specialized in the designing and production of bar code readers, mobile computers, sensors for detection, measurement and safety, RFID, vision and laser marking systems. Its cutting-edge solutions help to increase the efficiency and quality of processes in the Retail, Manufacturing, ...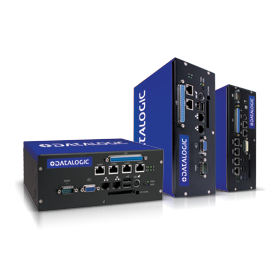
Vision Processors | MX Series
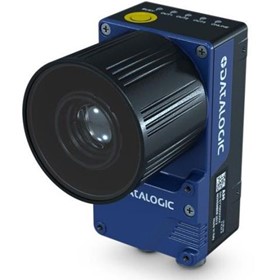
Rugged Machine Vision Camera | A30 Series

Omron Automation & Robotics is an Machine Vision Camera supplier to All
At Omron, we deal with our customers on the basis of a trusting relationship. As a world leader in automation control we have a broad capacity to provide systems and solutions using a diverse range of products and components. The Oceania region covers a vast distance incorporating Australia, New Zealand, Papua New Guinea and the islands of the South Pacific. From micro-relays ...
Inspection Systems is an Machine Vision Camera supplier to All
Established in 1997, Inspection Systems has developed a reputation for providing high performance systems, comprehensive support and specialist advice to the food and pharmaceutical manufacturing industry in Australia and New Zealand. Our customers include many of the world’s leading manufacturers, who choose Inspection Systems to help them comply with government regulations ...
KPM TheiaVu™ Benchtop Vision System

KPM EyePro Vision System

- Resolution: The camera resolution determines the level of detail in the image. A higher resolution camera will provide more detail, but may also require more processing power and storage space.
- Frame rate: The frame rate of the camera determines how many images can be captured per second. A higher frame rate is important for applications where motion needs to be captured accurately.
- Sensor size: The size of the camera's sensor affects the field of view and light sensitivity of the camera. Larger sensors generally provide better image quality and low-light performance.
- Pixel size: The size of the camera's pixels affects the camera's sensitivity to light and noise. Smaller pixels provide higher resolution, but may suffer from increased noise levels.
- Lens compatibility: The camera should be compatible with a range of lenses to provide flexibility in capturing images at various distances and angles.
- Connectivity: The camera should have a range of connectivity options to allow for easy integration with other hardware and software systems.
- CCD sensors typically have better image quality, lower noise, and higher sensitivity than CMOS sensors. They also have a global shutter, which means that all pixels are read out simultaneously, resulting in less distortion of moving objects.
- CMOS sensors, on the other hand, are generally less expensive and consume less power than CCD sensors. They also have a rolling shutter, which means that each row of pixels is read out sequentially, resulting in potential distortion of moving objects. However, newer CMOS sensors are being developed with a global shutter, which can improve their performance.
- Fixed focal length lenses are the most basic type of lens and provide a fixed magnification and field of view. They are suitable for applications where the object distance and size are consistent. Zoom lenses, on the other hand, offer variable magnification and field of view, making them ideal for applications where the object distance and size vary.
- Telecentric lenses are designed to minimize perspective errors by ensuring that the rays of light entering the lens are parallel to the optical axis. They are commonly used in applications where accurate measurements are critical. Wide-angle lenses, as the name suggests, provide a wider field of view and are typically used in applications where a large area needs to be captured.
- Some of the key factors that should be considered when selecting lighting for a machine vision system include:
- Type of application: Different applications may require different types of lighting, such as diffuse or direct lighting. For instance, if the application involves inspecting reflective surfaces, diffuse lighting may be the best option.
- Object being inspected: The object being inspected will also influence the choice of lighting. For example, if the object has a complex shape, shadowless lighting may be the best option.
- Camera being used: The camera being used will also play a role in selecting the right lighting. Different cameras may require different types of lighting to achieve optimal results.
- Environment: The environment in which the system operates will also influence the choice of lighting. For instance, if the system is operating in a dusty or humid environment, sealed lighting may be required.
- Color temperature: The color temperature of the lighting can also have an impact on the accuracy of the system. It is important to choose lighting with the appropriate color temperature for the application.
- Image Processing: The camera should be equipped with powerful image processing capabilities to analyze the images captured by the camera. This includes features such as image filtering, edge detection, and image enhancement.
- Image Analysis: The camera should be able to perform complex image analysis tasks such as object recognition, pattern matching, and defect detection. This requires advanced algorithms and machine learning capabilities.
- Calibration: The camera should be capable of accurate calibration to ensure precise measurements and consistent results.
- Integration: The camera should be easy to integrate with other software and hardware systems, such as industrial automation systems and programmable logic controllers (PLCs).
- User Interface: The camera should have an intuitive user interface that allows users to easily set up and configure the camera, as well as monitor and analyze the images captured by the camera.
- Connectivity: The camera should be designed to work with a variety of communication protocols such as Ethernet, USB, and GigE, to allow for easy data transfer and connectivity with other devices.
Machine Vision Camera Costs and Supplier Insights
If you are looking to buy a Machine Vision Camera for sale, suppliers on IndustrySearch include Diverseco, Micromax, Portable Analytical Solutions Pty Ltd
Why choose a supplier in Melbourne for Machine Vision Camera Quotes?
If you are in Melbourne and considering purchasing a Machine Vision Camera, it's worth considering Melbourne-based suppliers. Doing so offers several benefits that are particularly relevant to businesses in the area. Here are the top reasons why opting for a local Melbourne supplier can be the best decision for your Machine Vision Camera buying needs.
Streamlined ComplianceStreamline your compliance efforts by purchasing Machine Vision Camera from Melbourne. Local suppliers understand local legal landscapes, making compliance straightforward.
Create More Jobs in MelbourneCreate and keep jobs in Melbourne by buying your Machine Vision Camera from local suppliers. You'll help the job market and support local families.
Continuous Support for Your Machine Vision CameraGet continuous support for your Machine Vision Camera needs from Melbourne's local suppliers. Ongoing help ensures your equipment performs at its best.
Personalised Machine Vision Camera ConfigurationsBenefit from personalised Machine Vision Camera configurations available exclusively through select local suppliers.
Stay Ahead in Machine Vision Camera TechnologyStay ahead in Machine Vision Camera technology with the help of local suppliers. They bring the newest advancements directly to your doorstep, keeping you competitive.
Buying in Melbourne and Strengthen Your NetworkStrengthen your local business network by buying Machine Vision Camera in Melbourne. Connect with other businesses and foster community ties through local transactions.
Buy a Machine Vision Camera Near Me
 Reach valuable industrial buyers in minutes
 Promote key products & content
 Drive cost effective & measurable sales