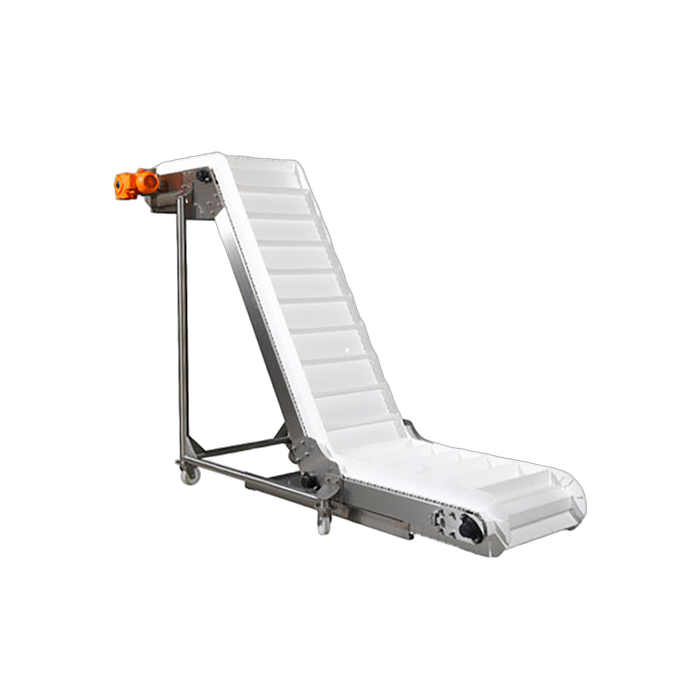
Conveyor System
Join industrial buyers comparing supplier quotes and buying with confidence. Free, quick and easy.





How IndustrySearch works
Tell us what you need
Answer a few quick questions about the equipment you're looking for.
Get personalised quotes
Receive tailored quotes from relevant Australian suppliers.
Compare and choose
Compare quotes, ask questions and choose the best option for you.
 Save time
 Compare quotes
 Buy with confidence
Save time, compare quotes & buy with confidence
Conveyor System Suppliers
Do you need to improve your production line efficiency and reliability? VEQTOR specialise in the design and manufacture of high quality conveyors, palletising solutions, pallet handling, industrial automation and more. Whether you need to upgrade your machines or start fresh, we have the expertise to deliver cost effective solutions that will increase your facility’s productivity, ...
Customers: Laminex, Vesco Foods, Orora, Geraldton Fishing Co-Op, V&V Walsh
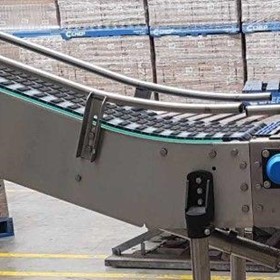
AmbaFlex is the partner for customized material handling systems based on spiral conveying technology! Vertical conveying and spiral accumulation are our specialties and our products are used all over the world. Our unique SpiralVeyor® is used in a wide range of markets and applications for vertical transportation, temporary storage and the accumulation of single goods and ...
Customers: P&G, Unilever, Mondelez, Nestlé, Ferrero, Amazon

Conveyor Systems AmbaVeyor AFa
Conveyor Systems | Elevator AmbaFlex BaggageLift
Conveyor Systems SpiralVeyor J-configuration | Spiral Conveyors
Conveyor Systems SpiralVeyor ML-configuration | Spiral Conveyors

Conveyor Systems Accuveyor-avl-series

Conveyor Systems AmbaVeyor Curved Solutions

MayTec boasts the largest range of profiles and accessories making it the most comprehensive and flexible slotted profile system in the world. Additionally MayTec Australia can provide services such as cutting, drilling, assembly and installation of orders. Products can be ordered in virtually any way you may require them - from fully designed and installed to bulk quantity ...


Cost effective and efficent warehouse/industrial storage solutions and equipment. New & Used Pallet Racking - all brands including Colby, Dexion, Schaeffer, Acrow and Spacerack. Raised Storage Areas, Shelving, Warehouse Storage Systems and Materials Handling Equipment. With a multitude of ways to optimise space for efficient storage, our expertise in the design, supply, ...
With more than 150 branches across Australia and New Zealand, Kennards Hire is Australia’s #1 family-owned supplier of high quality, equipment for hire.


Tenova TAKRAF is a competent partner for the development, planning, design, manufacture and supply of machines and technological plants of all kind, in particular plants, systems and equipment in the area of open cast mining and bulk materials handling. Our bulk material handling equipment is utilised in ports, stockyards, power stations, steel making plants, in the cement industry ...

AFS is a turnkey solutions provider for the Agriculture, Food & Seed industries. We specialise in the ‘3 Cs’ – CRUSH, CONVEY, CONTROL – offering a comprehensive range of highly efficient and cost-effective automated solutions tailored to your specific operation. Is your business looking to implement or upgrade to a well-planned, competitively priced and robust product / material ...

RAM Conveyors is a locally owned Australian supplier of bulk materials handling equipment. The business was originally established in 2014 to supply conveyor products / parts to Original Equipment Manufacturers, re-sellers and service companies. ?Today, RAM Conveyor's component supply skills are complemented by mechanical and rubber trades to service and support conveyor ...


A modular aluminium system for a wide range of applications, including Automation, Machine Guards, Safety Guarding, Trolleys, Work Bench Systems, Display Cabinets, Display Stands and Conveyors, using t-slot principles. • Custom made to suit your specific needs and dimensions • Flexible and modifiable for today’s ever-changing workplace • Huge range of products • Clean and ...


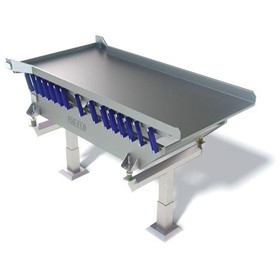
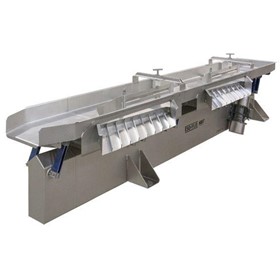
In the words of Key Technology co-founder Claude Key, “opportunity was everywhere” when he helped found the company in 1948. Since then, Key Technology has become a worldwide leader in food processing technology, continually striving to find and fulfill our customers’ growing needs. Our ongoing innovations provide increased control, continuous processing and longer machine ...
Conveyor System Buying Guide
Buy the best conveyor belts and conveying systems available from verified IndustrySearch suppliers. You’ll find quality brands perfect for bulk material or packaged product use including conveyor belts, chain conveyor, screw conveyor, spiral food conveyors and roller conveyor systems. Read our conveyor buying guide to help you choose your ideal conveyor system.

- Conveyor systems are an essential part of many industries, including manufacturing, warehousing, and transportation. They are used to move materials from one location to another quickly and efficiently, and can be customized to fit a variety of applications. Here are some factors to consider when selecting the best conveyor system for your industry or application:
- Material Type: The type of material being conveyed will determine the type of conveyor system needed. For example, heavy-duty materials may require a conveyor with a more robust design, while delicate materials may require a gentler conveyor system.
- Distance: The distance that the material must be transported will determine the length of the conveyor needed. Longer distances may require more power to move the materials, which may require a more robust conveyor system.
- Speed: The speed at which the materials need to be transported will also determine the type of conveyor system needed. For example, high-speed conveyors may require more power and a more robust design to ensure safe and efficient transportation.
- Space: The amount of space available in your facility will also impact the type of conveyor system you can use. For example, if space is limited, you may need to consider a vertical conveyor system or an overhead conveyor.
- Budget: Finally, your budget will also play a role in determining the best conveyor system for your application. Conveyor systems can range in price from a few thousand dollars to several hundred thousand dollars, depending on the complexity and size of the system.
- Site preparation: The site where the conveyor system will be installed needs to be cleared and leveled. Any obstructions or debris should be removed.
- Conveyor layout design: The layout design of the conveyor system should be finalized before installation begins. This includes determining the length, width, and height of the conveyor, as well as the location and size of any curves, inclines, or declines.
- Conveyor assembly: The conveyor system is assembled in sections or modules, which are then connected together. The assembly process may involve welding, bolting, or other methods of joining the sections.
- Conveyor installation: The assembled conveyor system is then installed on site. This involves positioning the conveyor sections in place and securing them to the floor or other support structures.
- Electrical and mechanical connections: Once the conveyor system is installed, electrical and mechanical connections are made to power and control the system. This includes connecting motors, sensors, and other components, as well as programming any control systems.
- Testing and commissioning: The conveyor system is then tested to ensure it is operating correctly and meets all safety and performance requirements. Any issues are addressed, and the system is commissioned for use.
- Emergency stop buttons: These are strategically placed along the conveyor system and can be used to immediately shut down the system in case of an emergency.
- Guarding: Physical barriers, fencing, or shielding can be installed to prevent employees from accessing dangerous areas of the conveyor system.
- Warning systems: Visual and audible warning systems can be installed to alert employees of potential hazards.
- Lockout/tagout procedures: These procedures ensure that the conveyor system is properly locked and tagged before maintenance or repair work is carried out.
- Automatic shut-off: Sensors or other technology can be used to automatically shut off the conveyor system if an object or person becomes trapped or stuck.
Conveyor System Costs and Supplier Insights
If you are looking to buy a Conveyor System for sale, suppliers on IndustrySearch include Veqtor, AmbaFlex Spiral Conveyor Solutions
Buy a Conveyor System Near Me
Conveyor System Articles & Reviews
-
![]() Buying guide
Belt Conveyor vs Roller Conveyor: Which System Fits Your Operation in 2026 ? in Conveyor-system
Read guide
-
![]() Buying guide
The real ROI of basic warehouse automation for Australian businesses in Conveyor-system
Read guide
-
![]() Buying guide
Conveyor system buying guide Australia: Types, prices, maintenance, compliance and more in Conveyor-system
Read guide
-
![]() Buying guide
Spiral Conveyor Prices in Australia: Buying Guide for Types, Features, Installation & Compliance in Conveyor-system
Read guide
-
![]() Buying guide
Case Packer Price & Buying Guide in Conveyor-system
Read guide
-
![]() Buying guide
Checkweigher Buying Guide: Prices, Features, and Key Considerations in Conveyor-system
Read guide


 Reach valuable industrial buyers in minutes
 Promote key products & content
 Drive cost effective & measurable sales