Rotary Blow Molding Machine | EBS 4 ERGON ...
Rotary Blow Molding Machine | EBS 4 ERGON


Rotary stretch-blow-moulders with output rate up to 8,800 bph (0.5 L)
After applying it to secondary packaging machines, SMI extended the ERGON design concept to its stretch-blow moulders and launched a brand-new machine series called EBS (Electronic Blowing System) ERGON, where advanced electronics took the lion’s share in the complete redesign of the entire equipment. The EBS ERGON project is based upon all-electronic processes which allow to get rid of the whole of mechanical movements and related cams and ultimately make the blower a cam-less machine.
The new range is composed of 7 models, from 4 to 16 cavities, suitable for the production of bottles up to 3 litres, with a maximum output of 2,100/2,200 bph/cavity (0.5 L containers).
The EBS ERGON series of rotary stretch blow-molders ensures high performances in the stretch blow-molding of PET, PEN and PP bottles, mainly used in the “food & beverage” sector. Thanks to high-tech components, minimized maintenance and operational costs and excellent quality/price ratio, the EBS ERGON series is the ideal solution for the production of plastic containers of different capacities, featuring various shapes, from the most simple to the most sophisticated ones.
Operation:
- Preforms feeding
The preforms are transferred from the hopper to the unscrambler through a lifting belt; the unscrambler conveys them to an inclined guide, from where they reach the spacer star wheel at the heating module infeed, by gravitational fall. The star wheel feeds the rotary mandrel chain, through which the preforms are “captured” and let into the heating module. - Preforms heating
Before entering the heating module, equipped with infrared lamps, each preform undergoes accurate checks, which detect its size and vertical position and automatically eliminate the preforms not compliant with the pre-set parameters. The preforms, supported by the mandrels, start moving along the heating module. During the heating process, the preforms constantly turn around themselves, so as to ensure an excellent and symmetrical heat distribution. The heating module is equipped with two different cooling systems: a liquid-fed cooling system, in order to cool the protection ring preventing the preforms thread deformation during the heating process; an air-fed cooling system, in order to keep the temperature inside the heating module as low as to avoid the exposure of the preforms outside walls to too high temperatures. At the heating module outlet, a sensor detects the preform temperature and compares it with the temperature set point; if the two values do not correspond, it increases or decreases the heating module lamps power. - Preform stretch blow-molding
A special rotary group of grippers picks up the preforms from the oven and sets them into the stretch-blowing stations. The stretch-blowing process includes two phases:
– stretching and pre-blowing, which occur simultaneously through the descent of the motorized stretching rod and the supply of low-pressure compressed air;
– final blowing with high-pressure compressed air, through which the containers take their final shape. A counter-pressure air system ensures the perfect locking of the moulds, whereas the mechanical locking of the mold-holders allows bearing the strengths generated by the stretch-blow moulding process with the maximum reliability. Also the stretch-blowing stations are equipped with a liquid-fed cooling system, which keeps the molds temperature constant. - Bottles outlet
During the blowing process, an accurate measurement system checks that the process follows the pression profile required. In fact, a pressure drop would alter the container shape which would cause the automatic rejection of the container. The finished bottles are picked from the stretch-blowing stations by another rotary group of grippers and put onto an air conveyor which finally transfers them to the filling machines.
* The stated values are not binding, as they have to be confirmed by SMI according to the user’s production conditions.
Technical Data
- PREFORMS UNSCRAMBLER
- recovery of the preforms in excess, carried back to the hopper
- GRIPPERS’ ROTARY GROUPS
- positively actuated valve gear control of the grippers rotary groups, by means of a double cam.
- PREFORM-HEATING MODULE
- horizontally positioned infrared lamps, grouped in various sections
- up to 8 infrared lamps for each section of the heating module
- possibility to set and modify the parameters of each lamp through the POSYC operator panel
- preform heating lengthwise differentiated and radially homogeneous
- heat-reflecting panels, made of composite material, mounted on the front and at the rear of the infra-red lamps to increase radiation intensity and, consequently, cut energy consumption
- mandrels chain pitch to 37 mm
- liquid-fed cooling system, in order to cool the protection ring preventing the preforms thread deformation during the heating process
- air-fed cooling system, in order to keep the heating module temperature constant and low enough
- modular design, standardized for all stretch blow-molders models
- STRETCH-BLOWING WHEEL
- standardized stretch-blowing stations for all blow-molders models, with a low dead volume thanks to high performance valves and optimized circuits
- liquid-fed cooling system, in order to keep the molds temperature constant
- air recovery system supplied as a standard equipment
- molds treated on the surface and made from a special aluminium alloy highly resistant to wear
- mold-holders made from an austempered iron casting highly resistant to mechanical stress
- motorized stretching rod to boost speed and enable a more flexible management of the stretching process
- AIR RECOVERY SYSTEM
- two exhaust valves for each stretch-blowing station: the first one introduces the air into the air recovery system tank, the second one discharges the air that can not be recycled
- considerable reduction of the energy costs and 40% saving in the compressed air consumption; thanks to the recovery system, a part of the air in the blowing circuit is recovered and recycled for the pre-blowing circuit and for the machine service air. The pressure of the pre-blowing circuit is controlled by an electronic adjusting device. If the pre-blowing circuit or the service air circuit do not need the recycled air, it is possible to use it for the low-pressure circuit of other external systems.
- use of eco-compatible, environment-friendly technology
- ELECTRICAL PANEL AND MACHINE WIRING
- electrical panel integrated in the heating module, thus reducing the machine overall dimensions; as a consequence, the final user has got larger space to install any optional equipment or additional accessories. Moreover, the machine structure is more compact and the access to it is easier, thanks to the elimination of the power cables (air or ground cables) that are generally used for the connection with the external electrical panels
- use of pre-assembled and pre-tested cables
- ethernet communication ring
- SERCOS interface™ field bus
* The stated values are not binding, as they have to be confirmed by SMI according to the user’s production conditions.
To contact SMIG about Rotary Blow Molding Machine | EBS 4 ERGON use Get a quote.
After applying it to secondary packaging machines, SMI extended the ERGON design concept to its stretch-blow moulders and launched a brand-new machine series called EBS (Electronic Blowing System) ERGON, where advanced electronics took the lion’s share in the complete redesign of the entire equipment. The EBS ERGON project is based upon all-electronic processes which allow to get rid of the whole of mechanical movements and related cams and ultimately make the blower a cam-less machine.
The new range is composed of 7 models, from 4 to 16 cavities, suitable for the production of bottles up to 3 litres, with a maximum output of 2,100/2,200 bph/cavity (0.5 L containers).
The EBS ERGON series of rotary stretch blow-molders ensures high performances in the stretch blow-molding of PET, PEN and PP bottles, mainly used in the “food & beverage” sector. Thanks to high-tech components, minimized maintenance and operational costs and excellent quality/price ratio, the EBS ERGON series is the ideal solution for the production of plastic containers of different capacities, featuring various shapes, from the most simple to the most sophisticated ones.
Operation:
- Preforms feeding
The preforms are transferred from the hopper to the unscrambler through a lifting belt; the unscrambler conveys them to an inclined guide, from where they reach the spacer star wheel at the heating module infeed, by gravitational fall. The star wheel feeds the rotary mandrel chain, through which the preforms are “captured” and let into the heating module. - Preforms heating
Before entering the heating module, equipped with infrared lamps, each preform undergoes accurate checks, which detect its size and vertical position and automatically eliminate the preforms not compliant with the pre-set parameters. The preforms, supported by the mandrels, start moving along the heating module. During the heating process, the preforms constantly turn around themselves, so as to ensure an excellent and symmetrical heat distribution. The heating module is equipped with two different cooling systems: a liquid-fed cooling system, in order to cool the protection ring preventing the preforms thread deformation during the heating process; an air-fed cooling system, in order to keep the temperature inside the heating module as low as to avoid the exposure of the preforms outside walls to too high temperatures. At the heating module outlet, a sensor detects the preform temperature and compares it with the temperature set point; if the two values do not correspond, it increases or decreases the heating module lamps power. - Preform stretch blow-molding
A special rotary group of grippers picks up the preforms from the oven and sets them into the stretch-blowing stations. The stretch-blowing process includes two phases:
– stretching and pre-blowing, which occur simultaneously through the descent of the motorized stretching rod and the supply of low-pressure compressed air;
– final blowing with high-pressure compressed air, through which the containers take their final shape. A counter-pressure air system ensures the perfect locking of the moulds, whereas the mechanical locking of the mold-holders allows bearing the strengths generated by the stretch-blow moulding process with the maximum reliability. Also the stretch-blowing stations are equipped with a liquid-fed cooling system, which keeps the molds temperature constant. - Bottles outlet
During the blowing process, an accurate measurement system checks that the process follows the pression profile required. In fact, a pressure drop would alter the container shape which would cause the automatic rejection of the container. The finished bottles are picked from the stretch-blowing stations by another rotary group of grippers and put onto an air conveyor which finally transfers them to the filling machines.
* The stated values are not binding, as they have to be confirmed by SMI according to the user’s production conditions.
Technical Data
- PREFORMS UNSCRAMBLER
- recovery of the preforms in excess, carried back to the hopper
- GRIPPERS’ ROTARY GROUPS
- positively actuated valve gear control of the grippers rotary groups, by means of a double cam.
- PREFORM-HEATING MODULE
- horizontally positioned infrared lamps, grouped in various sections
- up to 8 infrared lamps for each section of the heating module
- possibility to set and modify the parameters of each lamp through the POSYC operator panel
- preform heating lengthwise differentiated and radially homogeneous
- heat-reflecting panels, made of composite material, mounted on the front and at the rear of the infra-red lamps to increase radiation intensity and, consequently, cut energy consumption
- mandrels chain pitch to 37 mm
- liquid-fed cooling system, in order to cool the protection ring preventing the preforms thread deformation during the heating process
- air-fed cooling system, in order to keep the heating module temperature constant and low enough
- modular design, standardized for all stretch blow-molders models
- STRETCH-BLOWING WHEEL
- standardized stretch-blowing stations for all blow-molders models, with a low dead volume thanks to high performance valves and optimized circuits
- liquid-fed cooling system, in order to keep the molds temperature constant
- air recovery system supplied as a standard equipment
- molds treated on the surface and made from a special aluminium alloy highly resistant to wear
- mold-holders made from an austempered iron casting highly resistant to mechanical stress
- motorized stretching rod to boost speed and enable a more flexible management of the stretching process
- AIR RECOVERY SYSTEM
- two exhaust valves for each stretch-blowing station: the first one introduces the air into the air recovery system tank, the second one discharges the air that can not be recycled
- considerable reduction of the energy costs and 40% saving in the compressed air consumption; thanks to the recovery system, a part of the air in the blowing circuit is recovered and recycled for the pre-blowing circuit and for the machine service air. The pressure of the pre-blowing circuit is controlled by an electronic adjusting device. If the pre-blowing circuit or the service air circuit do not need the recycled air, it is possible to use it for the low-pressure circuit of other external systems.
- use of eco-compatible, environment-friendly technology
- ELECTRICAL PANEL AND MACHINE WIRING
- electrical panel integrated in the heating module, thus reducing the machine overall dimensions; as a consequence, the final user has got larger space to install any optional equipment or additional accessories. Moreover, the machine structure is more compact and the access to it is easier, thanks to the elimination of the power cables (air or ground cables) that are generally used for the connection with the external electrical panels
- use of pre-assembled and pre-tested cables
- ethernet communication ring
- SERCOS interface™ field bus
* The stated values are not binding, as they have to be confirmed by SMI according to the user’s production conditions.
To contact SMIG about Rotary Blow Molding Machine | EBS 4 ERGON use Get a quote.
Calculating...
SMI’s EBS 4 ERGON is a rotary stretch-blow-moulding machine that forms plastic preforms into bottles. Its cam-less, all-electronic operation removes mechanical movements and their associated cams from the blowing machine. Food and beverage producers can use it to make PET bottles in different capacities and shapes, ranging from simple containers to more complex bottle designs.
- Air recovery recycles blowing-circuit air for pre-blowing and machine service
- Air recovery: 40% compressed-air saving, subject to confirmation for production conditions
- Up to 8 infrared lamps per heating section
- POSYC operator panel sets and adjusts each lamp’s parameters
- Preforms outside preset size or vertical-position parameters are automatically rejected
Source: listing by SMIG on IndustrySearch · Updated 2 Nov 2026
AI Overview is generated by artificial intelligence and may contain mistakes.
Written by AI from the listing by SMIG on IndustrySearch. It is meant to use only what that listing says, but it can still get details wrong, so check them with the supplier before you buy.
Thanks for your feedback.
- Your delivery location?
- NSW
- VIC
- QLD
- SA
- WA
- NT
- ACT
- TAS
- New Zealand
- Papua New Guinea
- Afghanistan
- Albania
- Algeria
- Andorra
- Angola
- Antigua and Barbuda
- Argentina
- Armenia
- Austria
- Azerbaijan
- Bahamas
- Bahrain
- Bangladesh
- Barbados
- Belarus
- Belgium
- Belize
- Benin
- Bhutan
- Bolivia
- Bosnia and Herzegovina
- Botswana
- Brazil
- Brunei
- Bulgaria
- Burkina Faso
- Burma
- Burundi
- Cabo Verde
- Cambodia
- Cameroon
- Canada
- Central African Republic
- Chad
- Chile
- China
- Colombia
- Comoros
- Congo (Brazzaville)
- Congo (Kinshasa)
- Costa Rica
- Côte d'Ivoire
- Croatia
- Cuba
- Cyprus
- Czechia
- Denmark
- Djibouti
- Dominica
- Dominican Republic
- Ecuador
- Egypt
- El Salvador
- Equatorial Guinea
- Eritrea
- Estonia
- Ethiopia
- Fiji
- Finland
- France
- Gabon
- Gambia
- Georgia
- Germany
- Ghana
- Greece
- Grenada
- Guatemala
- Guinea
- Guinea-Bissau
- Guyana
- Haiti
- Holy See
- Honduras
- Hungary
- Iceland
- India
- Indonesia
- Iran
- Iraq
- Ireland
- Israel
- Italy
- Jamaica
- Japan
- Jordan
- Kazakhstan
- Kenya
- Kiribati
- Korea, North
- Korea, South
- Kosovo
- Kuwait
- Kyrgyzstan
- Laos
- Latvia
- Lebanon
- Lesotho
- Liberia
- Libya
- Liechtenstein
- Lithuania
- Luxembourg
- Macedonia
- Madagascar
- Malawi
- Malaysia
- Maldives
- Mali
- Malta
- Marshall Islands
- Mauritania
- Mauritius
- Mexico
- Federated States of Micronesia
- Moldova
- Monaco
- Mongolia
- Montenegro
- Morocco
- Mozambique
- Namibia
- Nauru
- Nepal
- Netherlands
- New Zealand
- Nicaragua
- Niger
- Nigeria
- Norway
- Oman
- Pakistan
- Palau
- Panama
- Papua New Guinea
- Paraguay
- Peru
- Philippines
- Poland
- Portugal
- Qatar
- Romania
- Russia
- Rwanda
- Saint Kitts and Nevis
- Saint Lucia
- Saint Vincent and the Grenadines
- Samoa
- San Marino
- Sao Tome and Principe
- Saudi Arabia
- Senegal
- Serbia
- Seychelles
- Sierra Leone
- Singapore
- Slovakia
- Slovenia
- Solomon Islands
- Somalia
- South Africa
- South Sudan
- Spain
- Sri Lanka
- Sudan
- Suriname
- Swaziland
- Sweden
- Switzerland
- Syria
- Taiwan
- Tajikistan
- Tanzania
- Thailand
- Timor-Leste
- Togo
- Tonga
- Trinidad and Tobago
- Tunisia
- Turkey
- Turkmenistan
- Tuvalu
- Uganda
- Ukraine
- United Arab Emirates
- United Kingdom
- United States
- Uruguay
- Uzbekistan
- Vanuatu
- Venezuela
- Vietnam
- Yemen
- Zambia
- Zimbabwe
- NSW
- VIC
- QLD
- SA
- WA
- NT
- ACT
- TAS
- New Zealand
- Papua New Guinea
- Afghanistan
- Albania
- Algeria
- Andorra
- Angola
- Antigua and Barbuda
- Argentina
- Armenia
- Austria
- Azerbaijan
- Bahamas
- Bahrain
- Bangladesh
- Barbados
- Belarus
- Belgium
- Belize
- Benin
- Bhutan
- Bolivia
- Bosnia and Herzegovina
- Botswana
- Brazil
- Brunei
- Bulgaria
- Burkina Faso
- Burma
- Burundi
- Cabo Verde
- Cambodia
- Cameroon
- Canada
- Central African Republic
- Chad
- Chile
- China
- Colombia
- Comoros
- Congo (Brazzaville)
- Congo (Kinshasa)
- Costa Rica
- Côte d'Ivoire
- Croatia
- Cuba
- Cyprus
- Czechia
- Denmark
- Djibouti
- Dominica
- Dominican Republic
- Ecuador
- Egypt
- El Salvador
- Equatorial Guinea
- Eritrea
- Estonia
- Ethiopia
- Fiji
- Finland
- France
- Gabon
- Gambia
- Georgia
- Germany
- Ghana
- Greece
- Grenada
- Guatemala
- Guinea
- Guinea-Bissau
- Guyana
- Haiti
- Holy See
- Honduras
- Hungary
- Iceland
- India
- Indonesia
- Iran
- Iraq
- Ireland
- Israel
- Italy
- Jamaica
- Japan
- Jordan
- Kazakhstan
- Kenya
- Kiribati
- Korea, North
- Korea, South
- Kosovo
- Kuwait
- Kyrgyzstan
- Laos
- Latvia
- Lebanon
- Lesotho
- Liberia
- Libya
- Liechtenstein
- Lithuania
- Luxembourg
- Macedonia
- Madagascar
- Malawi
- Malaysia
- Maldives
- Mali
- Malta
- Marshall Islands
- Mauritania
- Mauritius
- Mexico
- Federated States of Micronesia
- Moldova
- Monaco
- Mongolia
- Montenegro
- Morocco
- Mozambique
- Namibia
- Nauru
- Nepal
- Netherlands
- New Zealand
- Nicaragua
- Niger
- Nigeria
- Norway
- Oman
- Pakistan
- Palau
- Panama
- Papua New Guinea
- Paraguay
- Peru
- Philippines
- Poland
- Portugal
- Qatar
- Romania
- Russia
- Rwanda
- Saint Kitts and Nevis
- Saint Lucia
- Saint Vincent and the Grenadines
- Samoa
- San Marino
- Sao Tome and Principe
- Saudi Arabia
- Senegal
- Serbia
- Seychelles
- Sierra Leone
- Singapore
- Slovakia
- Slovenia
- Solomon Islands
- Somalia
- South Africa
- South Sudan
- Spain
- Sri Lanka
- Sudan
- Suriname
- Swaziland
- Sweden
- Switzerland
- Syria
- Taiwan
- Tajikistan
- Tanzania
- Thailand
- Timor-Leste
- Togo
- Tonga
- Trinidad and Tobago
- Tunisia
- Turkey
- Turkmenistan
- Tuvalu
- Uganda
- Ukraine
- United Arab Emirates
- United Kingdom
- United States
- Uruguay
- Uzbekistan
- Vanuatu
- Venezuela
- Vietnam
- Yemen
- Zambia
- Zimbabwe

Calculating...
SMI Cooling Conveyors
Wrap Around Case Packers | WP 400
Ergon Automatic Packers | LCM 30
Ergon Multi Lane Dividers | DV 250 S
Automatic Shrink Wrapping Machine | AFW 30 ERGON
APS 3100L P Ergon Palletiser
APS 1550 P ERGON Palletiser
Stretch Blow Molding, Filling & Capping Machine | ECOBLOC
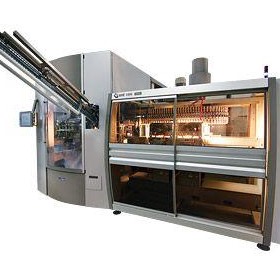
Rotary Blow Molding Machine | EBS 4 ERGON
Blow Moulding Machines for Plastics
Injection Blow Molding Machine (Bottle Making Machine) ZC30F
Injection Blow Molding Machine (Bottle Making Machine) ZC60B
Injection Blow Molding Machine (Bottle Making Machine) IBM30H
Injection Blow Molding Machine (Bottle Making Machine) IBM50H
Injection Blow Molding Machine (Bottle Making Machine) IBM80H
Blow Moulding Machinery
Stretch Blow Molding, Filling & Capping Machine | ECOBLOC
Blow Moulding Machines
Blow Moulding Machine | Contiform 3 Pro
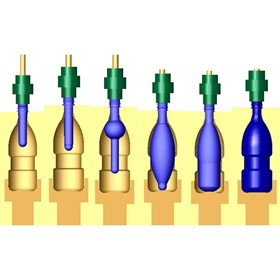
Stretch Blow Moulding Machine
Blow Moulding Machine
Blow Fill Lines | Icon Equipment

SIPA Blow Moulding Machine
Thanks for your help!
Sorry! Unable to submit your request at this time. Please try again later.
Report this product
 Reach valuable industrial buyers in minutes
 Promote key products & content
 Drive cost effective & measurable sales