Stretch Blow Molding, Filling & Capping ...
Stretch Blow Molding, Filling & Capping Machine | ECOBLOC
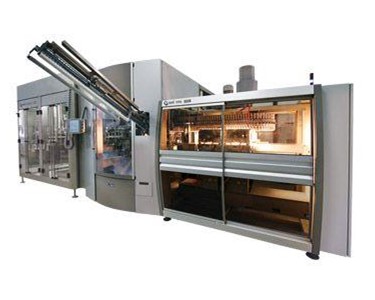

ECOBLOC® ERGON LG-VMAG - Stretch-blow moulding, filling and capping integrated system with output rate up to 33,600 bph (0.5 L)
The integrated system of stretch-blow moulding, filling and capping of the ECOBLOC® ERGON LG-VMAG series combines the functions of a rotary stretch-blow moulder, of an electronic rotary filler and of a rotary capper.
The ECOBLOC® integrated system stands out for:
- compact modular frame, with a wide choice of customization options;
- latest technology innovations adopted in the machine design;
- perfect synchronization between the “dry” environment of the stretch-blow moulding module and the “wet” environment of the filling module;
- minimum number of transfer star wheels, as the stretch-blow moulding module and the filling/capping module stand ”back to back”, with no need for connecting conveyors;
- operating and maintenance costs dramatically cut;
- outstanding price/quality ratio.
SMI’s ECOBLOC® ERGON LG-VMAG series models are the ideal solution for manufacturing, filling and capping PET, PEN and PP containers of many different sizes and shapes, from the simplest to the most complex and innovative. Combining stretch-blow moulding, filling and capping in one single machine offers major economic benefits:
- no need for a rinser, accumulation conveyors and conveyors between the blower and the filler;
- virtual elimination of container contamination risks;
- considerable reduction of line inefficiency causes;
All models are equipped with an innovative bottle transfer system, minimizing the risks of product contamination and increasing the machine’s overall performance; ECOBLOC® ERGON LG-VMAG integrated systems can be employed in the bottling lines of the following products:
- SPARKLING WATER
- CARBONATED SOFT DRINKS
Operation:
- Preforms Feeding
- The preforms are transferred from the hopper to the unscrambler through a lifting belt; the unscrambler conveys them to an inclined guide, from where they reach the spacer star wheel at the heating module infeed, by gravitational fall. The star wheel feeds the rotary mandrel chain, through which the preforms are “captured” and let into the heating module.
- Preforms Heating
- Before entering the heating module, equipped with infrared lamps, each preform undergoes accurate checks, which detect its size and vertical position and automatically eliminate the preforms not compliant with the pre-set parameters. The preforms, supported by the mandrels, start moving along the heating module. During the heating process, the preforms constantly turn around themselves, so as to ensure an excellent and symmetrical heat distribution. The heating module is equipped with two different cooling systems: a liquid-fed cooling system, in order to cool the protection ring preventing the preforms thread deformation during the heating process; an air-fed cooling system, in order to keep the temperature inside the heating module as low as to avoid the exposure of the preforms outside walls to too high temperatures. At the heating module outlet, a sensor detects the preform temperature and compares it with the temperature set point; if the two values do not correspond, it increases or decreases the heating module lamps power.
- Preform Stretch Blow Moulding
- A special rotary group of grippers picks up the preforms from the oven and sets them into the stretch-blowing stations. The stretch-blowing process includes two phases:
– stretching and pre-blowing, which occur simultaneously through the descent of the motorized stretching rod and the supply of low-pressure compressed air;
– final blowing with high-pressure compressed air, through which the containers take their final shape. A counter-pressure air system ensures the perfect locking of the moulds, whereas the mechanical locking of the mold-holders allows bearing the strengths generated by the stretch-blow moulding process with the maximum reliability. Also the stretch-blowing stations are equipped with a liquid-fed cooling system, which keeps the molds temperature constant.
- A special rotary group of grippers picks up the preforms from the oven and sets them into the stretch-blowing stations. The stretch-blowing process includes two phases:
- Bottles Outlet
- During the blowing process, an accurate measurement system checks that the process follows the pression profile required. In fact, a pressure drop would alter the container shape which would cause the automatic rejection of the container. The finished bottles are picked from the stretch-blowing stations by another rotary group of grippers and put onto an air conveyor which finally transfers them to the filling machines.
- Empty Bottles Transfer
- After being manufactured by the stretch-blowing module (see EBS ERGON), empty bottles are conveyed from the blower to the filler by “neck-handling” direct transfer through a starwheel-starwheel system. The star-wheel at the blowmoulder outlet is equipped with grippers electronically synchronised with the brackets of the starwheel at the filler inlet.
- Electronic Filling
- A sensor detects the presence of the bottle at the filler inlet; the filling process starts only if a bottle is detected. The product to be bottled is fed from a small external tank to the filling valves by means of a pump or by gravity in the case of foam products. The filling process is electronic volumetric with magnetic flow-meters (VMAG models for conductive products) or electronic massic with mass meters based on the Coriolis’ principle (VMAS models for nonconductive products). A flowmeter positioned upstream of each filling valve gauges the amount of product flowing through. The flow amount is gauged by pulses-counting: upon reaching the set amount of pulses for the current format, a signal is sent to the filling valve to be closed.
- Pick & Place Capping System
- Full bottles are transferred to the capper by means of a star-wheel equipped with grippers. Caps are oriented in the correct position by a hopper-unscrambler standing outside the machine at an easy-access height, and are transferred to a pick & place device positioning the cap under the capping head, which moves downwards and applies the cap on the bottle.
* The stated values are not binding, as they have to be confirmed by SMI according to the user’s production conditions.
Benefits:
- modular compact frame, offering a wide array of customization options;
- perfect separation between the “dry” environment of the stretchblow moulding module and the “wet” environment of the filling module;
- the “Baseless” technology employed allows for a minimum number of transfer star-wheels and for easier access to the blower and to the filler for maintenance and cleaning operations;
- direct bottle transfer by means of adjoining star-wheels (neckhandling style with pitch circle diameter);
- the integrated system – excluding both rinser and connecting conveyors – drives down energy and water consumption;
- dramatic cutback of TCO;
- use of eco-friendly technologies, for the safeguard of the environment;
- high cleanliness and hygiene standards;
- excellent quality-price ratio.
The Filling Module
The “Baseless” technology employed on the filling module features the following benefits:
- area underneath the bottles completely clear, so as to ease the operator’s access to the machine for maintenance and cleaning operations;
- lower maintenance and intervention times;
- contamination-free and high-hygiene environment;
- motors and transmissions placed in the upper part of the machine, in a dry and easy-to-inspect area;
- dummy bottle system, for CIP operations.
Electronic Filling
ECOBLOC® integrated systems employ exclusively state-of-the-art filling technologies, with the following benefits:
- fully electronic management of the filling cycle;
- filling parameters selection from the operator panel, according to product, container, speed;
- simple-design, ready-to-clean filling valves;
- easy and quick format changeover, with no need to replace mechanical components.
Electronic volumetric filling – ECOBLOC® VMAG/VMAS: FLAT LIQUIDS
- magnetic flow-meters, for flat conductive products (> 30 uS/ cm), such as STILL WATER and MILK;
- massic flow-meters, for flat nonconductive products (< 30 uS/ cm), such as STILL WATER and EDIBLE OIL;
- The flowmeter gauges the quantity of product (volume or mass) flowing through the pipe feeding the filling valve and turns it into pulses.
- Upon reaching a given number of pulses, the filling process stops.
Isobaric electronic volumetric filling – ECOBLOC® LG-VMAG: CARBONATED LIQUIDS
- Magnetic flowmeters, for carbonated conductive products (> 30 uS/cm) such as SPARKLING WATER and CSDs
- The flowmeter gauges the quantity of product (volume or mass) flowing through the pipe feeding the filling valve and turns it into pulses.
- Upon reaching a given number of pulses, the filling process stops.
The Capping Module
- high precision system, for the application of screw caps and pressure caps;
- external cap feeding hopper;
- shorter intervention time in case of cap jamming;
- water-fall cap feeder-orienter (optional) which delivers caps conveniently oriented to the feeding channel;
- no more centrifugal hopper with relevant cap jamming hazard (optional);
- no more air thrust (optional).
* The stated values are not binding, as they have to be confirmed by SMI according to the user’s production conditions.
To contact SMIG about Stretch Blow Molding, Filling & Capping Machine | ECOBLOC use Get a quote.
The integrated system of stretch-blow moulding, filling and capping of the ECOBLOC® ERGON LG-VMAG series combines the functions of a rotary stretch-blow moulder, of an electronic rotary filler and of a rotary capper.
The ECOBLOC® integrated system stands out for:
- compact modular frame, with a wide choice of customization options;
- latest technology innovations adopted in the machine design;
- perfect synchronization between the “dry” environment of the stretch-blow moulding module and the “wet” environment of the filling module;
- minimum number of transfer star wheels, as the stretch-blow moulding module and the filling/capping module stand ”back to back”, with no need for connecting conveyors;
- operating and maintenance costs dramatically cut;
- outstanding price/quality ratio.
SMI’s ECOBLOC® ERGON LG-VMAG series models are the ideal solution for manufacturing, filling and capping PET, PEN and PP containers of many different sizes and shapes, from the simplest to the most complex and innovative. Combining stretch-blow moulding, filling and capping in one single machine offers major economic benefits:
- no need for a rinser, accumulation conveyors and conveyors between the blower and the filler;
- virtual elimination of container contamination risks;
- considerable reduction of line inefficiency causes;
All models are equipped with an innovative bottle transfer system, minimizing the risks of product contamination and increasing the machine’s overall performance; ECOBLOC® ERGON LG-VMAG integrated systems can be employed in the bottling lines of the following products:
- SPARKLING WATER
- CARBONATED SOFT DRINKS
Operation:
- Preforms Feeding
- The preforms are transferred from the hopper to the unscrambler through a lifting belt; the unscrambler conveys them to an inclined guide, from where they reach the spacer star wheel at the heating module infeed, by gravitational fall. The star wheel feeds the rotary mandrel chain, through which the preforms are “captured” and let into the heating module.
- Preforms Heating
- Before entering the heating module, equipped with infrared lamps, each preform undergoes accurate checks, which detect its size and vertical position and automatically eliminate the preforms not compliant with the pre-set parameters. The preforms, supported by the mandrels, start moving along the heating module. During the heating process, the preforms constantly turn around themselves, so as to ensure an excellent and symmetrical heat distribution. The heating module is equipped with two different cooling systems: a liquid-fed cooling system, in order to cool the protection ring preventing the preforms thread deformation during the heating process; an air-fed cooling system, in order to keep the temperature inside the heating module as low as to avoid the exposure of the preforms outside walls to too high temperatures. At the heating module outlet, a sensor detects the preform temperature and compares it with the temperature set point; if the two values do not correspond, it increases or decreases the heating module lamps power.
- Preform Stretch Blow Moulding
- A special rotary group of grippers picks up the preforms from the oven and sets them into the stretch-blowing stations. The stretch-blowing process includes two phases:
– stretching and pre-blowing, which occur simultaneously through the descent of the motorized stretching rod and the supply of low-pressure compressed air;
– final blowing with high-pressure compressed air, through which the containers take their final shape. A counter-pressure air system ensures the perfect locking of the moulds, whereas the mechanical locking of the mold-holders allows bearing the strengths generated by the stretch-blow moulding process with the maximum reliability. Also the stretch-blowing stations are equipped with a liquid-fed cooling system, which keeps the molds temperature constant.
- A special rotary group of grippers picks up the preforms from the oven and sets them into the stretch-blowing stations. The stretch-blowing process includes two phases:
- Bottles Outlet
- During the blowing process, an accurate measurement system checks that the process follows the pression profile required. In fact, a pressure drop would alter the container shape which would cause the automatic rejection of the container. The finished bottles are picked from the stretch-blowing stations by another rotary group of grippers and put onto an air conveyor which finally transfers them to the filling machines.
- Empty Bottles Transfer
- After being manufactured by the stretch-blowing module (see EBS ERGON), empty bottles are conveyed from the blower to the filler by “neck-handling” direct transfer through a starwheel-starwheel system. The star-wheel at the blowmoulder outlet is equipped with grippers electronically synchronised with the brackets of the starwheel at the filler inlet.
- Electronic Filling
- A sensor detects the presence of the bottle at the filler inlet; the filling process starts only if a bottle is detected. The product to be bottled is fed from a small external tank to the filling valves by means of a pump or by gravity in the case of foam products. The filling process is electronic volumetric with magnetic flow-meters (VMAG models for conductive products) or electronic massic with mass meters based on the Coriolis’ principle (VMAS models for nonconductive products). A flowmeter positioned upstream of each filling valve gauges the amount of product flowing through. The flow amount is gauged by pulses-counting: upon reaching the set amount of pulses for the current format, a signal is sent to the filling valve to be closed.
- Pick & Place Capping System
- Full bottles are transferred to the capper by means of a star-wheel equipped with grippers. Caps are oriented in the correct position by a hopper-unscrambler standing outside the machine at an easy-access height, and are transferred to a pick & place device positioning the cap under the capping head, which moves downwards and applies the cap on the bottle.
* The stated values are not binding, as they have to be confirmed by SMI according to the user’s production conditions.
Benefits:
- modular compact frame, offering a wide array of customization options;
- perfect separation between the “dry” environment of the stretchblow moulding module and the “wet” environment of the filling module;
- the “Baseless” technology employed allows for a minimum number of transfer star-wheels and for easier access to the blower and to the filler for maintenance and cleaning operations;
- direct bottle transfer by means of adjoining star-wheels (neckhandling style with pitch circle diameter);
- the integrated system – excluding both rinser and connecting conveyors – drives down energy and water consumption;
- dramatic cutback of TCO;
- use of eco-friendly technologies, for the safeguard of the environment;
- high cleanliness and hygiene standards;
- excellent quality-price ratio.
The Filling Module
The “Baseless” technology employed on the filling module features the following benefits:
- area underneath the bottles completely clear, so as to ease the operator’s access to the machine for maintenance and cleaning operations;
- lower maintenance and intervention times;
- contamination-free and high-hygiene environment;
- motors and transmissions placed in the upper part of the machine, in a dry and easy-to-inspect area;
- dummy bottle system, for CIP operations.
Electronic Filling
ECOBLOC® integrated systems employ exclusively state-of-the-art filling technologies, with the following benefits:
- fully electronic management of the filling cycle;
- filling parameters selection from the operator panel, according to product, container, speed;
- simple-design, ready-to-clean filling valves;
- easy and quick format changeover, with no need to replace mechanical components.
Electronic volumetric filling – ECOBLOC® VMAG/VMAS: FLAT LIQUIDS
- magnetic flow-meters, for flat conductive products (> 30 uS/ cm), such as STILL WATER and MILK;
- massic flow-meters, for flat nonconductive products (< 30 uS/ cm), such as STILL WATER and EDIBLE OIL;
- The flowmeter gauges the quantity of product (volume or mass) flowing through the pipe feeding the filling valve and turns it into pulses.
- Upon reaching a given number of pulses, the filling process stops.
Isobaric electronic volumetric filling – ECOBLOC® LG-VMAG: CARBONATED LIQUIDS
- Magnetic flowmeters, for carbonated conductive products (> 30 uS/cm) such as SPARKLING WATER and CSDs
- The flowmeter gauges the quantity of product (volume or mass) flowing through the pipe feeding the filling valve and turns it into pulses.
- Upon reaching a given number of pulses, the filling process stops.
The Capping Module
- high precision system, for the application of screw caps and pressure caps;
- external cap feeding hopper;
- shorter intervention time in case of cap jamming;
- water-fall cap feeder-orienter (optional) which delivers caps conveniently oriented to the feeding channel;
- no more centrifugal hopper with relevant cap jamming hazard (optional);
- no more air thrust (optional).
* The stated values are not binding, as they have to be confirmed by SMI according to the user’s production conditions.
To contact SMIG about Stretch Blow Molding, Filling & Capping Machine | ECOBLOC use Get a quote.
Calculating...
The ECOBLOC ERGON LG-VMAG combines stretch-blow moulding, filling and capping in one machine, with output up to 33,600 bph (0.5 L), subject to SMI confirmation for your production conditions. Its neck-handling transfer moves bottles between adjoining star wheels, removing the need for connecting conveyors. Bottlers of sparkling water and carbonated soft drinks can use its isobaric electronic volumetric filling for conductive products.
- Magnetic flowmeters measure conductive liquids above 30 uS/cm
- Format changes require no replacement of mechanical components
- Dummy bottle system for CIP operations
- Applies screw caps and pressure caps
- Optional water-fall cap feeder-orienter delivers caps in the correct orientation
Source: listing by SMIG on IndustrySearch · Updated 31 Oct 2026
AI Overview is generated by artificial intelligence and may contain mistakes.
Written by AI from the listing by SMIG on IndustrySearch. It is meant to use only what that listing says, but it can still get details wrong, so check them with the supplier before you buy.
Thanks for your feedback.
- Your delivery location?
- NSW
- VIC
- QLD
- SA
- WA
- NT
- ACT
- TAS
- New Zealand
- Papua New Guinea
- Afghanistan
- Albania
- Algeria
- Andorra
- Angola
- Antigua and Barbuda
- Argentina
- Armenia
- Austria
- Azerbaijan
- Bahamas
- Bahrain
- Bangladesh
- Barbados
- Belarus
- Belgium
- Belize
- Benin
- Bhutan
- Bolivia
- Bosnia and Herzegovina
- Botswana
- Brazil
- Brunei
- Bulgaria
- Burkina Faso
- Burma
- Burundi
- Cabo Verde
- Cambodia
- Cameroon
- Canada
- Central African Republic
- Chad
- Chile
- China
- Colombia
- Comoros
- Congo (Brazzaville)
- Congo (Kinshasa)
- Costa Rica
- Côte d'Ivoire
- Croatia
- Cuba
- Cyprus
- Czechia
- Denmark
- Djibouti
- Dominica
- Dominican Republic
- Ecuador
- Egypt
- El Salvador
- Equatorial Guinea
- Eritrea
- Estonia
- Ethiopia
- Fiji
- Finland
- France
- Gabon
- Gambia
- Georgia
- Germany
- Ghana
- Greece
- Grenada
- Guatemala
- Guinea
- Guinea-Bissau
- Guyana
- Haiti
- Holy See
- Honduras
- Hungary
- Iceland
- India
- Indonesia
- Iran
- Iraq
- Ireland
- Israel
- Italy
- Jamaica
- Japan
- Jordan
- Kazakhstan
- Kenya
- Kiribati
- Korea, North
- Korea, South
- Kosovo
- Kuwait
- Kyrgyzstan
- Laos
- Latvia
- Lebanon
- Lesotho
- Liberia
- Libya
- Liechtenstein
- Lithuania
- Luxembourg
- Macedonia
- Madagascar
- Malawi
- Malaysia
- Maldives
- Mali
- Malta
- Marshall Islands
- Mauritania
- Mauritius
- Mexico
- Federated States of Micronesia
- Moldova
- Monaco
- Mongolia
- Montenegro
- Morocco
- Mozambique
- Namibia
- Nauru
- Nepal
- Netherlands
- New Zealand
- Nicaragua
- Niger
- Nigeria
- Norway
- Oman
- Pakistan
- Palau
- Panama
- Papua New Guinea
- Paraguay
- Peru
- Philippines
- Poland
- Portugal
- Qatar
- Romania
- Russia
- Rwanda
- Saint Kitts and Nevis
- Saint Lucia
- Saint Vincent and the Grenadines
- Samoa
- San Marino
- Sao Tome and Principe
- Saudi Arabia
- Senegal
- Serbia
- Seychelles
- Sierra Leone
- Singapore
- Slovakia
- Slovenia
- Solomon Islands
- Somalia
- South Africa
- South Sudan
- Spain
- Sri Lanka
- Sudan
- Suriname
- Swaziland
- Sweden
- Switzerland
- Syria
- Taiwan
- Tajikistan
- Tanzania
- Thailand
- Timor-Leste
- Togo
- Tonga
- Trinidad and Tobago
- Tunisia
- Turkey
- Turkmenistan
- Tuvalu
- Uganda
- Ukraine
- United Arab Emirates
- United Kingdom
- United States
- Uruguay
- Uzbekistan
- Vanuatu
- Venezuela
- Vietnam
- Yemen
- Zambia
- Zimbabwe
- NSW
- VIC
- QLD
- SA
- WA
- NT
- ACT
- TAS
- New Zealand
- Papua New Guinea
- Afghanistan
- Albania
- Algeria
- Andorra
- Angola
- Antigua and Barbuda
- Argentina
- Armenia
- Austria
- Azerbaijan
- Bahamas
- Bahrain
- Bangladesh
- Barbados
- Belarus
- Belgium
- Belize
- Benin
- Bhutan
- Bolivia
- Bosnia and Herzegovina
- Botswana
- Brazil
- Brunei
- Bulgaria
- Burkina Faso
- Burma
- Burundi
- Cabo Verde
- Cambodia
- Cameroon
- Canada
- Central African Republic
- Chad
- Chile
- China
- Colombia
- Comoros
- Congo (Brazzaville)
- Congo (Kinshasa)
- Costa Rica
- Côte d'Ivoire
- Croatia
- Cuba
- Cyprus
- Czechia
- Denmark
- Djibouti
- Dominica
- Dominican Republic
- Ecuador
- Egypt
- El Salvador
- Equatorial Guinea
- Eritrea
- Estonia
- Ethiopia
- Fiji
- Finland
- France
- Gabon
- Gambia
- Georgia
- Germany
- Ghana
- Greece
- Grenada
- Guatemala
- Guinea
- Guinea-Bissau
- Guyana
- Haiti
- Holy See
- Honduras
- Hungary
- Iceland
- India
- Indonesia
- Iran
- Iraq
- Ireland
- Israel
- Italy
- Jamaica
- Japan
- Jordan
- Kazakhstan
- Kenya
- Kiribati
- Korea, North
- Korea, South
- Kosovo
- Kuwait
- Kyrgyzstan
- Laos
- Latvia
- Lebanon
- Lesotho
- Liberia
- Libya
- Liechtenstein
- Lithuania
- Luxembourg
- Macedonia
- Madagascar
- Malawi
- Malaysia
- Maldives
- Mali
- Malta
- Marshall Islands
- Mauritania
- Mauritius
- Mexico
- Federated States of Micronesia
- Moldova
- Monaco
- Mongolia
- Montenegro
- Morocco
- Mozambique
- Namibia
- Nauru
- Nepal
- Netherlands
- New Zealand
- Nicaragua
- Niger
- Nigeria
- Norway
- Oman
- Pakistan
- Palau
- Panama
- Papua New Guinea
- Paraguay
- Peru
- Philippines
- Poland
- Portugal
- Qatar
- Romania
- Russia
- Rwanda
- Saint Kitts and Nevis
- Saint Lucia
- Saint Vincent and the Grenadines
- Samoa
- San Marino
- Sao Tome and Principe
- Saudi Arabia
- Senegal
- Serbia
- Seychelles
- Sierra Leone
- Singapore
- Slovakia
- Slovenia
- Solomon Islands
- Somalia
- South Africa
- South Sudan
- Spain
- Sri Lanka
- Sudan
- Suriname
- Swaziland
- Sweden
- Switzerland
- Syria
- Taiwan
- Tajikistan
- Tanzania
- Thailand
- Timor-Leste
- Togo
- Tonga
- Trinidad and Tobago
- Tunisia
- Turkey
- Turkmenistan
- Tuvalu
- Uganda
- Ukraine
- United Arab Emirates
- United Kingdom
- United States
- Uruguay
- Uzbekistan
- Vanuatu
- Venezuela
- Vietnam
- Yemen
- Zambia
- Zimbabwe

Calculating...
SMI Cooling Conveyors
Wrap Around Case Packers | WP 400
Ergon Automatic Packers | LCM 30
Ergon Multi Lane Dividers | DV 250 S
Automatic Shrink Wrapping Machine | AFW 30 ERGON
APS 3100L P Ergon Palletiser
APS 1550 P ERGON Palletiser
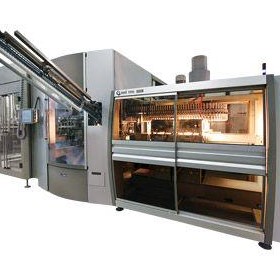
Stretch Blow Molding, Filling & Capping Machine | ECOBLOC
Rotary Blow Molding Machine | EBS 4 ERGON
Blow Moulding Machines for Plastics
Injection Blow Molding Machine (Bottle Making Machine) ZC30F
Injection Blow Molding Machine (Bottle Making Machine) ZC60B
Injection Blow Molding Machine (Bottle Making Machine) IBM30H
Injection Blow Molding Machine (Bottle Making Machine) IBM50H
Injection Blow Molding Machine (Bottle Making Machine) IBM80H
Blow Moulding Machinery
Rotary Blow Molding Machine | EBS 4 ERGON
Blow Moulding Machines
Blow Moulding Machine | Contiform 3 Pro
Stretch Blow Moulding Machine
Blow Moulding Machine
Blow Fill Lines | Icon Equipment

SIPA Blow Moulding Machine
Thanks for your help!
Sorry! Unable to submit your request at this time. Please try again later.
Report this product
 Reach valuable industrial buyers in minutes
 Promote key products & content
 Drive cost effective & measurable sales